ARNO - каталог сверление 2011
для размещения заказа - info@arno-tools.ru
Рекомендации по применению
Application reference
Donnes dapplication
SHARK-Drill2
2
Если для Вас этот инструмент новинка.
• Выбирайте по возможности самый короткий корпус.
• На странице 108 этого каталога Вы можете посмотреть рекомендуемые
режимы резания.
Данные рекомендации являются усредненными и не учитывают стабил
ность оборудования.
• Убедитесь в том, что корпус сверла надежно закреплен и соо с ность уст
новки сверла не более 0,02-0,04мм о. т центра.
• Проверьте, соответствует ли давление и расход охлаждающей жидко с сти соглас
но рекомендациям на стр. 111
• При сверлениии в плоскую повехность допускается врезание при максимальной подаче без предвари
тельного засверливания.
Наиболее точное отверстие Вы сможете получить при предварительном засврливаниии на вход е
при подаче 30-50% от базовой.
• При сверлении на глуби ну 1-2 x D необходимо проверить тружксообразование. Стружка не должна
быть с ливной и иметь синий оттенок. Синий цвет стружки означает чрезмерный перегрев
инструмента.
• Проверьте тестовое отверстие потребуемому допуску на округлость, шероховатость и
прямолинейность.
• В случае успешного предварительного засверливания продолжайте р аботу, незабывая проверять
качество отверстий после каждого цик ла.
New application? Never applied tool?
• Select the shortest possible drill for the application.
• On page 108 of this catalogue leaflet you can get cutting data recommendations. These are standard
recommendations in general. Stability of machine and component is not taken into account.
• Please ensure that the holder is securely fastened and its run out is maximum 0,02 - 0,04 mm to centre.
Please also check insert assembly (see guidelines page 112).
• Please check that coolant pressure is as recommended. High cutting data needs suitable coolant pressure. (see
page 111).
• If drilling into a flat surface you can pre-drill using full feed rate. An improved centring is obtained, when pre-drilling, by
reducing feed rate by 30-50%.
• Drill 1-2 x D deep. The swarf should be short (not stringy or blue).
• Stop and measure the hole tolerance, check the straightness and surface finish.
• If all is correct, continue drilling. Ensuring that the drilling operation runs smooth and soft cutting.
Nouvelle application? Jamais utilis?
• Choisissez l’outil le plus court pour l’application concerne
• Les valeurs de coupe sont indiques page 109 du catalogue. Il s’agit de valeurs standards pour la plupart des cas. La stabilit des machines et des
pices ne sont pas prisent en compte
• Assurez-vous que l’outil soit bien serr et qu’il tourne avec un faux rond de 0,02-0,04mm. Faire attention galement au montage de la plaquette (voir page 112)
• Vrifiez que la pression d’arrosage correspond aux recommandations indiques. Une valeur de coupe leve ncessite une pression d’arrosage adapte
(voir page 111)
• Effectuez un pr-perage pleine avance lors d’un perage d’une surface plane. Vous obtiendrez un meilleur centrage en rduisant l’avance de 30% 50%
• Effectuez ensuite un perage d’une profondeur d’environ 1-2xD. Les copeaux produits aprs la coupe doivent tre courts (pas filants ou bleuis)
• Arrtez puis mesurer le trou et vrifiez la tolrance. Vrifiez galement le centrage et l’tat de surface
• Continuez le perage si tout est correct. Assurez-vous que le processus de perage reste rgulier et sans -coups
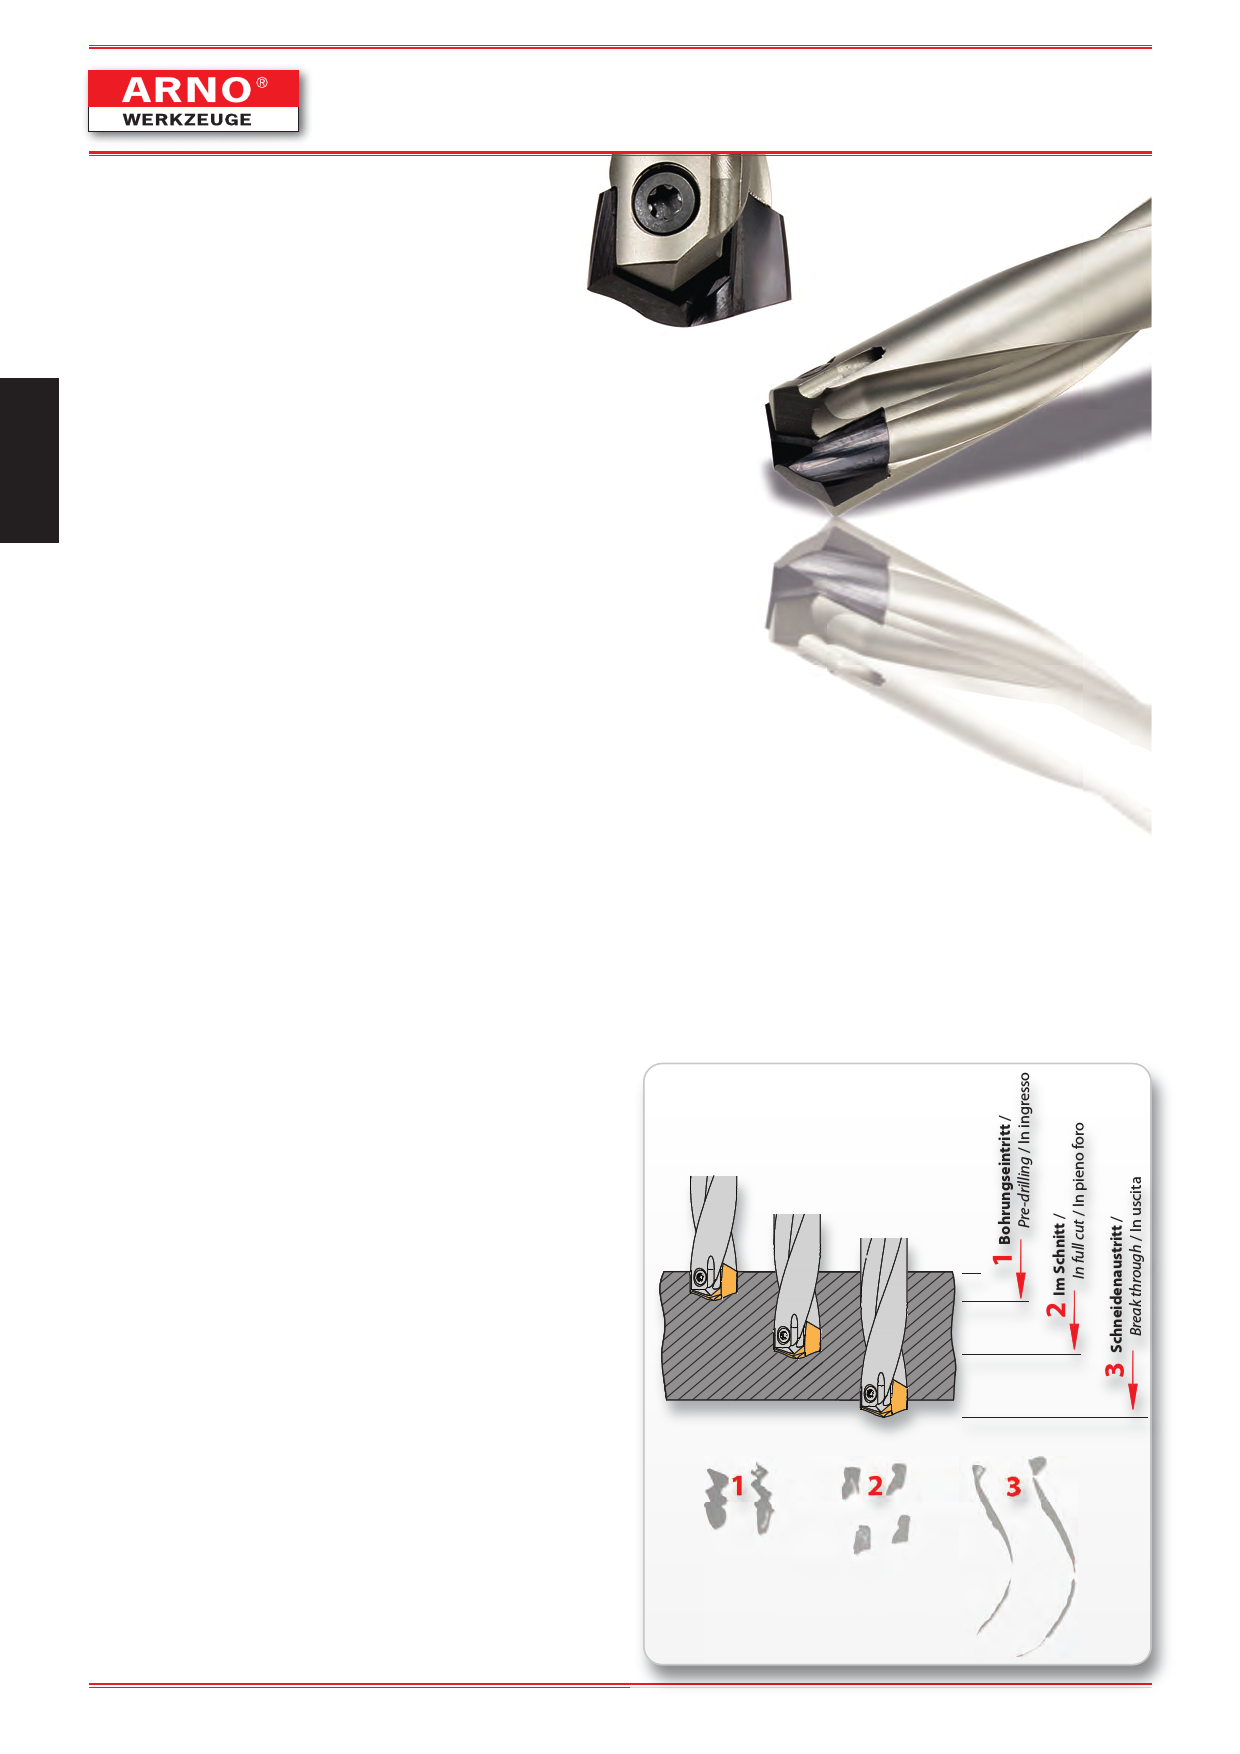
Стружкообразование >>
Формирование стружки на различных этапах сверления.
1. При пре дварительном засверлив ании и не д олжн о быть
длинн ой спир альн ой стружки
2. Этот тип стружки будет легко выводиться из отверстия
3. Длинная стружка может образовываться на выходе сверла, так
как на этом этапе режет только боковая часть пластины
Оптимизируйте параметры СОЖ при этой операции.
Swarf formation >>
Swarf shapes in every phase of drilling process:
1. Long spiral swarf does not interfere when pre-drilling.
2. This shape of swarf should easily and with a soft cutting sound be
evacuated from the hole.
3. Long swarf, as at the bottom of the hole, only the edges are cutting.
Optimize coolant pressure until drilling operation is completed.
Forme des copeaux >>
Forme des copeaux chaque phase de perage
1. Les copeaux longs en spirale ne gnent pas l’entre du perage
2. Ce genre de copeaux doit tre lger et s’vacuer avec fluidit
3. Copeaux longs obtenus la fin de l’avance lorsque que seule la
pointe coupe. Optimisez la pression d’arrosage jusqu’ ce que
l’opration de perage soit compltement termine
123
110
Размеры указаны в мм
Dimensions in mm
Toutes les dimensions en mm
info@arno-tools.ru
www.arno-tools.ru
110